Premium Product Showcase
Granular Activated Carbon
Granular Activated Carbon (GAC) is a highly porous adsorbent with a large surface area, engineered to effectively remove impurities, odors, colors, organic contaminants, and harmful compounds from liquids and gases. Available in various particle sizes and grades, GAC is widely used in water treatment, air purification, food & beverage processing, chemical industries, and industrial filtration.
Premium Product Showcase
Powdered Activated Carbon
Powdered Activated Carbon (PAC) is a highly porous, fine-grade adsorbent engineered for rapid and efficient purification. Its exceptionally high surface area enables fast removal of colour, odour, taste, organic contaminants and impurities from liquids and process streams.
CARBON KING offers high-performance PAC for water & wastewater treatment, food & beverage processing, pharmaceuticals, chemicals and industrial purification applications.
Premium Product Showcase
Pelletized Activated Carbon
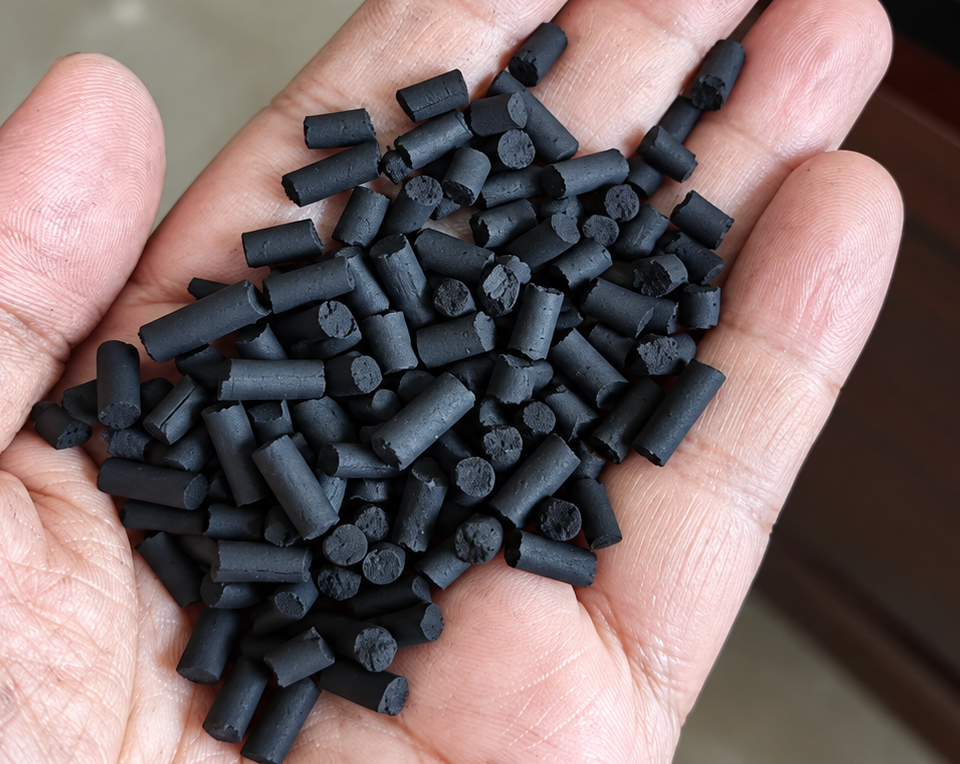
Pelletized Activated Carbon is a cylindrical, extruded adsorbent built for gas and vapour phase applications. Its uniform pellet shape gives low pressure drop and high mechanical strength, so deep beds stay efficient and predictable over long service runs.
CARBON KING supplies pelletized grades for air & gas purification, solvent recovery, VOC removal, flue gas treatment and industrial odour control.
Premium Product Showcase
Anthracite Coal
Our anthracite coal portfolio delivers tailored solutions for applications within the commercial, industrial, chemical and manufacturing industries. This premium, dark black coal is primarily employed for residential and commercial heating, waste treatment, and water filtration.
Characterized by a 40–90% carbon content and very low moisture and volatile matter, our anthracite coal offers clean combustion and high calorific value — making it an exceptional energy resource.